Internal Surface Roughness for Medical Stainless Steel Tubing: A Buyer Specification Guide
Why Internal Surface Roughness Needs Its Own Specification
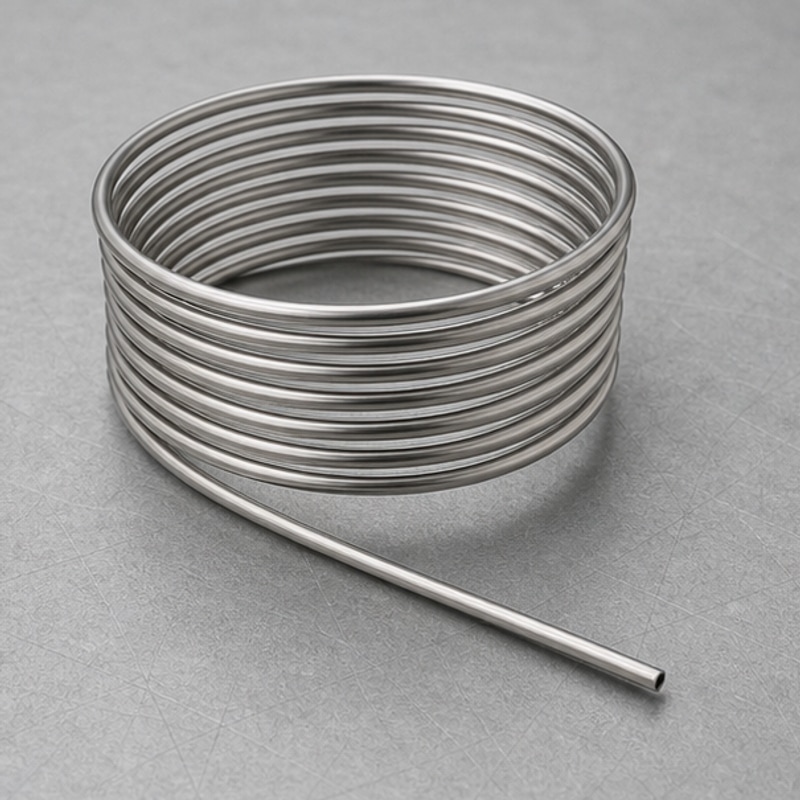
For small-diameter stainless steel tubing, buyers often define outside diameter, inside diameter, wall thickness and cut length but leave the internal surface described only as smooth or polished. Those words are open to interpretation. Two tubes can have similar dimensions and a similar visual appearance while showing different drawing lines, pits, oxide, embedded debris or local roughness inside the bore.
Internal surface condition may influence flow behavior, cleaning difficulty, residue retention, friction during component insertion and the consistency of downstream processes. The importance of each factor depends on the device design and intended use. A low roughness value by itself does not prove cleanliness, corrosion performance, biocompatibility or regulatory compliance. It is one controlled characteristic within a larger product specification.
A useful buyer specification therefore answers four separate questions: which surface parameter is controlled, where it is evaluated, how it is measured and what condition the tube must be in when delivered.
Ra Is Useful, but It Is Not a Complete Surface Description
Ra, the arithmetic average roughness, is commonly used because it gives one numerical summary of a measured profile. However, different profiles can produce similar Ra values. A surface with occasional deep defects may share an average value with a more uniform surface, even though the two surfaces behave differently in an assembly or cleaning process.
Depending on the application, a buyer may also need to consider maximum defects, waviness, directional drawing marks, pits, folds or another profile parameter such as Rz. The drawing should identify the selected parameter and the applicable measurement convention instead of assuming that every supplier uses the same cutoff, filter and evaluation length.
When a numerical roughness requirement is not justified by the device design, a controlled visual standard or approved reference sample may be more practical. The acceptance method should still be documented and repeatable.
Internal Diameter Creates a Measurement Challenge
The bore of a capillary tube may be too small for a conventional stylus instrument. Even when a probe can enter the tube, its tip geometry, travel direction and available evaluation length may not be suitable for the required measurement. Cutting the tube open can make the surface accessible, but sectioning and preparation can alter the area being inspected.
Possible approaches include a prepared longitudinal section, a cross-section, optical surface measurement, a replica method, a purpose-built internal probe or an agreed process coupon. No single method is appropriate for every ID, material, finish and tolerance. The RFQ should ask the supplier to state the proposed method and its limitations before the order is approved.
If destructive inspection is required, the buyer should define whether the tested sample comes from the same material lot and production run, and whether it represents the beginning, middle or end of the processed length.
Specify Location and Direction
A roughness requirement without a location can produce misleading results. Tube surfaces may vary along the length, near cut ends or after a secondary operation. The drawing or inspection plan should identify the measurement zone and whether end regions are excluded.
Direction also matters. A measurement taken parallel to drawing lines can differ from one taken across them. If the direction is important, state it. For long tubing, the buyer may require results from more than one longitudinal position. For formed, laser-cut or locally processed tubes, the inspection area should be related to the functional region.
Connect the Requirement to the Manufacturing Route
Cold drawing, annealing, straightening, cutting, mechanical polishing, chemical treatment and electropolishing can each affect the delivered surface. A supplier should not select a process only to achieve a headline roughness number. The route must also protect dimensions, wall uniformity, material condition and the required end geometry.
Mechanical polishing can reduce prominent marks but may be difficult to control inside a very small bore. Electropolishing can modify surface peaks and improve uniformity under suitable conditions, but its effect depends on alloy, geometry, electrical contact, solution control and starting surface. Passivation is different from electropolishing and should not be treated as a guaranteed roughness-reduction step.
Buyers comparing these options can review the existing Healsmed guides to capillary tube surface finishes and electropolishing and passivation for stainless steel capillary tubing.
What to Put on the Drawing or RFQ
| Specification item | Buyer decision | Why it matters |
|---|---|---|
| Surface | Internal, external or both | Prevents an external result from being used for an internal requirement |
| Parameter | Ra, Rz, defect limit or approved visual standard | Defines what is actually controlled |
| Limit and units | Maximum or range, stated in consistent units | Avoids unit conversion and acceptance disputes |
| Measurement method | Instrument or method approved for the bore size | Confirms the surface can be evaluated repeatably |
| Filter and evaluation conditions | Applicable cutoff, filter and evaluation length | Different settings can produce different results |
| Location | Distance from ends and positions along the tube | Accounts for variation along the manufactured length |
| Direction | Parallel, transverse or another defined orientation | Drawing marks can make direction significant |
| Sampling | Pieces, lots, positions and destructive samples | Links the result to production evidence |
| Delivered condition | As-drawn, annealed, polished, passivated, cleaned or packaged state | Ensures inspection represents the supplied product |
| Records | Certificate, raw data, images or inspection report | Defines what the buyer will receive and retain |
Roughness and Cleanliness Are Different Requirements
A smoother surface can be easier to clean in some applications, but a roughness report does not identify particles, oil, polishing compound, detergent residue or packaging contamination. Cleanliness should be specified and verified separately.
The buyer should state the cleaning stage, prohibited residues, handling expectations, packaging configuration and any test method required by the project. If parts will be cleaned again by the OEM, the incoming condition still needs an acceptance definition. For more detail, see the guide to cleanliness requirements for medical tubing.
Build a Practical Inspection Plan
An inspection plan should reflect both technical risk and measurement feasibility. It may include an initial qualification sample, periodic process verification, lot-based sampling or inspection after a process change. The supplier and buyer should agree how a destructive measurement represents the rest of the lot.
The report should identify the part number, drawing revision, material lot, production lot, sample location, instrument or method, calibration status, measurement settings, results and acceptance decision. When images are part of the evidence, include scale and location information rather than relying on an unlabeled photograph.
If the supplier uses a process coupon instead of the delivered tube, the buyer should understand how that coupon matches the actual alloy, starting condition, geometry and processing route. A coupon can support process monitoring, but it should not automatically replace product measurement when the bore geometry changes the finishing result.
Common Specification Mistakes
- Writing mirror finish without a numerical or visual acceptance method.
- Specifying an Ra limit without stating whether it applies to the ID, OD or both.
- Requiring stylus measurement where the probe cannot access the bore correctly.
- Comparing supplier results produced with different filters or evaluation lengths.
- Using one measurement near the tube end to represent the entire length.
- Assuming electropolishing, passivation and cleaning are interchangeable processes.
- Treating surface roughness as proof of cleanliness or medical compliance.
- Failing to define when a process or material change requires renewed approval.
Buyer Questions Before Quotation
- Can the proposed measurement method access the specified internal diameter?
- Will inspection be performed on the finished product, a cut sample or a process coupon?
- Which measurement settings and locations will appear on the report?
- How does the finishing route affect OD, ID and wall thickness?
- How are samples linked to the raw material and production lot?
- What cleaning and packaging condition follows the roughness inspection?
- Which changes would require a new qualification sample?
For a useful quotation, combine these answers with material, OD, ID, wall thickness, tolerance, cut length, quantity and intended application. The medical stainless steel capillary tube page provides the main capability overview.
Frequently Asked Questions
Does a lower Ra value automatically mean a better medical tube?
No. The appropriate value depends on the design and process. Dimensions, defects, cleanliness, material, end condition and downstream assembly requirements must also be controlled.
Can the external surface roughness represent the internal surface?
Not unless the buyer has established and approved a valid relationship for the specific manufacturing process. ID and OD surfaces can experience different tooling, contact and finishing conditions.
Should the requirement be measured before or after cleaning?
The drawing or inspection plan should define the delivered condition. Roughness is normally evaluated at an agreed production stage, while cleanliness is controlled separately on the finished delivered condition.
What if the internal diameter is too small to measure directly?
The buyer and supplier should agree on a qualified alternative such as destructive sectioning, optical evaluation, a replica method or a representative process coupon, and document the limitations of that approach.
Conclusion
A strong internal surface specification is more than one Ra number. It links the surface parameter to a measurable location, direction, method, sampling plan and delivered condition. That detail helps medical tubing buyers compare suppliers fairly and prevents inspection disagreements after production begins.
Send the drawing, bore size, target surface requirement and inspection expectations through the Healsmed RFQ page for manufacturability review.
Healsmed
Leading Stainless Steel Capillary Tube Factory. 1,400+ standard sizes IN STOCK & ready to ship worldwide! High precision, factory-direct price.