First Article Inspection for Custom Medical Tubing: An OEM Buyer Checklist
Why First Article Inspection Matters for Medical Tubing
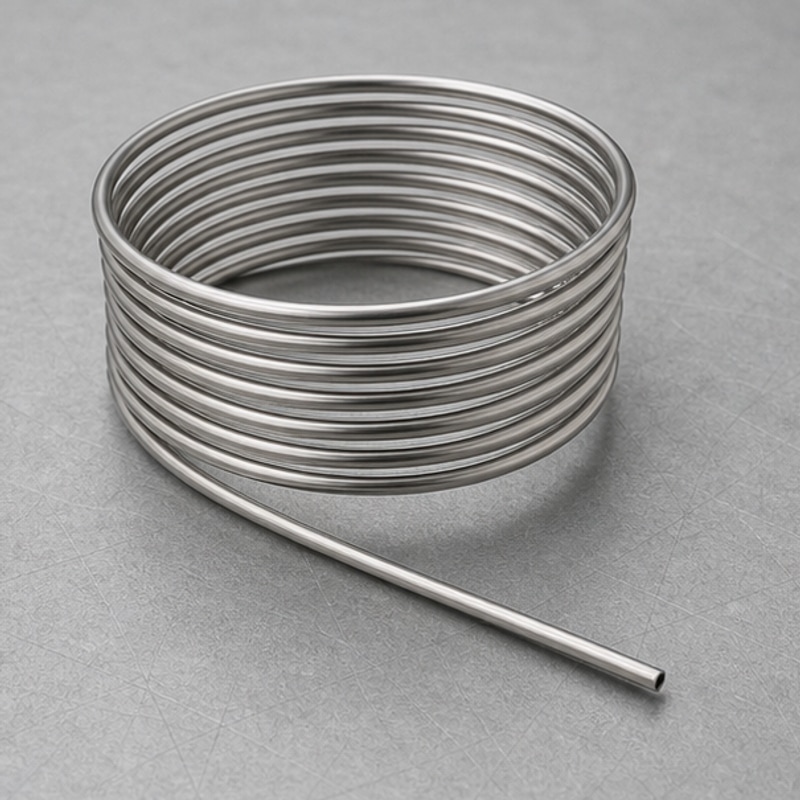
Custom medical tubing can look simple on a drawing, but a small change in outside diameter, inside diameter, wall thickness, cut length or end condition can affect assembly fit and downstream processing. A first article inspection, often shortened to FAI, gives the buyer and supplier a controlled checkpoint before routine production begins.
The purpose is not to prove that every future part will be acceptable. It is to confirm that the supplier understood the current drawing revision, selected an appropriate manufacturing route, used the specified material and can measure the characteristics that matter to the application. For an OEM buyer, a useful FAI package should connect each reported result to a drawing requirement and an identifiable sample.
FAI is also not a substitute for process validation, biological evaluation, sterilization validation or the medical device manufacturer’s regulatory responsibilities. Its role is narrower: verify the first production evidence against the agreed technical requirements.
When Should an OEM Request a New FAI?
The need for a new or partial FAI should be agreed during supplier qualification. Common triggers include:
- A new custom tube drawing or a first order from a new manufacturing source.
- A drawing revision that changes a dimension, tolerance, material, finish or inspection method.
- A change in forming, drawing, annealing, cutting, grinding, polishing or cleaning process.
- New tooling, a new production line or transfer to another manufacturing location.
- A material grade or approved material source change.
- A long production interruption when the buyer requires renewed evidence of capability.
- A corrective action where the affected characteristics need to be reverified.
Not every administrative drawing change needs a complete repeat inspection. The buyer and supplier should identify which characteristics are affected and document whether a full or partial FAI is appropriate.
Freeze the Drawing Revision Before Measuring
The most important FAI control is often document control. The purchase order, drawing, specification and inspection report must refer to the same revision. Before production, confirm the units, tolerances, datum references, surface requirements, sampling expectations and any notes that override general tolerances.
For tubing, an RFQ should normally define material grade, OD, ID or wall thickness, cut length, quantity, end condition, surface finish and intended application. When a dimension is derived, such as wall thickness calculated from OD and ID, the drawing should state which dimensions are directly controlled and which are reference values. This avoids a report that appears complete but does not match the design intent.
Critical Characteristics to Include
| Characteristic | What the buyer should define | Typical evidence |
|---|---|---|
| Material identity | Grade, specification and any source restrictions | Material certificate reference and lot identification |
| Outside diameter | Nominal size, tolerance and measurement locations | Recorded results with instrument identification |
| Inside diameter | Nominal size, tolerance and acceptable measurement method | Pin, optical, air-gauge or other agreed measurement result |
| Wall thickness | Minimum, maximum or concentricity requirement where applicable | Cross-section, ultrasonic or calculated evidence as agreed |
| Cut length | Length tolerance and reference points | Individual sample measurements |
| Straightness and geometry | Inspection span, datum and acceptance method | Fixture, optical or dimensional inspection record |
| End condition | Burr limit, chamfer, bevel, square cut or rounded end | Magnified images and dimensional checks where specified |
| Surface condition | Finish, visible defect criteria and roughness requirement if needed | Visual record and profilometer result when specified |
| Cleanliness and packaging | Cleaning state, particle controls and packaging configuration | Process record, inspection result and labeled package sample |
The measurement method must have suitable resolution for the tolerance. Buyers should not assume that the same instrument is appropriate for every tube size. Very small IDs, thin walls, flexible tubing and polished internal surfaces can require different measurement approaches. The supplier should state the instrument type and, where relevant, the inspection location or orientation.
Agree the Sample Plan and Report Format
An FAI sample quantity should reflect the drawing, manufacturing process and risk of the characteristic. There is no single sample count that fits every custom tube. The buyer should specify whether results are required for each submitted piece, whether samples must come from different positions in the production lot and whether destructive cross-section measurements are needed.
A practical report identifies the part number, part description, drawing revision, purchase order, material lot, production lot, sample identification, inspection date, measured value, requirement, result and inspection equipment. Ballooned drawing numbers can make the relationship between the drawing and report easier to review, especially when the tube includes slots, windows, formed ends or multiple secondary operations.
Material Traceability Must Follow the Samples
A material certificate alone does not establish complete traceability. The FAI package should show how the certificate reference connects to the raw tube lot and the submitted samples. When 304, 316L, titanium or another alloy is specified, the reported grade should match the drawing and purchase order exactly.
Buyers should also decide which records must remain available after approval. Depending on the project, these may include incoming material records, process route identification, in-process measurements, final inspection results and packaging labels. Retention periods and document language should be agreed contractually rather than assumed.
Do Not Overlook End Quality and Handling
Medical tubing often continues into laser cutting, forming, welding, bonding or assembly. A tube can meet OD and ID requirements but still create problems if the cut end has an uncontrolled burr, the lumen contains debris, the surface is scratched or the packaging allows tubes to rub during transport.
The FAI should therefore represent the condition in which production parts will actually be delivered. If the specification calls for deburring, cleaning, protective separation or capped ends, those requirements should be demonstrated on the submitted samples and recorded in the approval package.
Questions to Ask Before Approval
- Does the report reference the current drawing and purchase order revision?
- Can every result be traced to a specific submitted sample?
- Are all drawing characteristics accounted for, including notes and surface requirements?
- Are measurement methods suitable for the dimensions and tolerances?
- Is the material certificate connected to the production lot?
- Do sample ends, surfaces, cleanliness and packaging represent normal production?
- Are deviations clearly identified instead of being treated as accepted requirements?
- Is there an agreed rule for changes that require a new or partial FAI?
What to Send in the RFQ Package
To obtain a meaningful quotation and inspection plan, send the controlled drawing, material requirement, annual and order quantity, target tolerance, length, surface and end requirements, cleaning state, packaging expectation and required documentation. State whether FAI pricing and lead time should be separated from routine production.
Related buyer resources include the medical tubing RFQ checklist, the guide to medical tubing material certificates and the medical stainless steel capillary tube capability page.
Frequently Asked Questions
Is a first article sample the same as a prototype?
Not necessarily. A prototype may be produced with a temporary process to evaluate design intent. An FAI sample should represent the agreed production method closely enough to provide useful evidence before routine manufacturing.
Should every dimension be included in the FAI report?
The report should account for every applicable drawing requirement. If a characteristic is reference-only, not measurable on the submitted state or covered by another controlled record, the report should explain how it is addressed.
Can a material certificate replace dimensional inspection?
No. A material certificate supports alloy and lot information, while dimensional inspection verifies the manufactured geometry. Both may be required for a complete review.
What happens when an FAI result is outside tolerance?
The supplier should identify the nonconforming result and obtain written disposition before treating the sample as approved. The drawing should not be informally changed to match the part.
Conclusion
A useful first article inspection turns a drawing into verifiable production evidence. For custom medical tubing, the strongest packages connect revision control, material identity, dimensional results, end quality, surface condition and sample traceability. Buyers can use this checkpoint to resolve misunderstandings before they become repeated production problems.
To discuss a custom tubing project, send your drawing and inspection requirements through the Healsmed RFQ contact page.
Healsmed
Leading Stainless Steel Capillary Tube Factory. 1,400+ standard sizes IN STOCK & ready to ship worldwide! High precision, factory-direct price.