Straightness, Roundness and Ovality in Medical Stainless Steel Tubing: A Buyer Inspection Guide
Why Tube Geometry Needs More Than an OD Tolerance
A medical stainless steel tube can meet its stated outside diameter at one measurement point and still create assembly problems. A bowed length may not feed consistently into automated equipment. A locally oval section may not fit a mating component as expected. A round outside surface can also hide uneven wall thickness or an off-center bore.
Straightness, roundness and ovality describe different aspects of geometry. They should not be treated as interchangeable terms, and none of them is automatically controlled just because OD and ID limits are shown on a drawing. For an OEM buyer, the practical goal is to identify which geometric condition affects function and then define a repeatable way to inspect it.
There is no universal straightness or ovality value that is suitable for every medical tube. Material grade, diameter, wall thickness, temper, cut length, downstream processing, measurement force and end use all influence what can be manufactured and verified. The supplier should review the complete drawing before confirming capability.
Straightness, Roundness and Ovality Are Different
Straightness
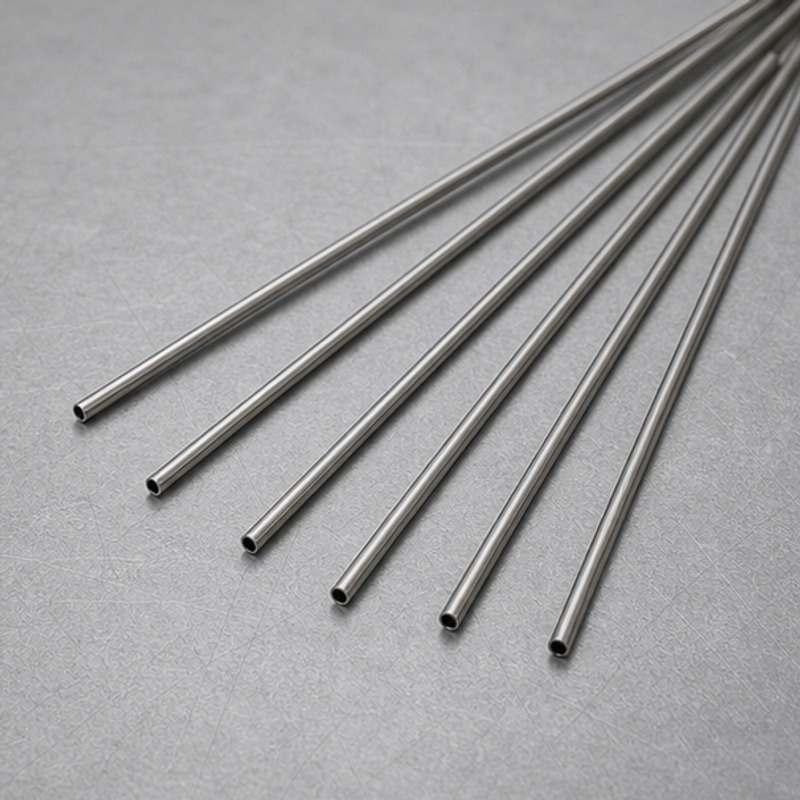
Straightness describes how much a line element or tube axis departs from the specified straight condition. For tubing, buyers often use the word to describe bow over a stated length. A meaningful requirement must identify the evaluation span, the reference condition and how the deviation is measured.
Roundness
Roundness, sometimes called circularity in formal geometric dimensioning, describes how closely one cross-section follows a true circle. It is a local form characteristic. It does not tell the buyer whether the full tube is straight, and it is not the same as checking only the largest and smallest diameter with a hand micrometer.
Ovality
Ovality is commonly expressed as the difference between the maximum and minimum diameters measured at one cross-section. Some specifications use an absolute value, while others divide that difference by the nominal or mean diameter and report a percentage. Because both conventions exist, the drawing must state the formula and units. A requirement that says only “ovality 2%” is incomplete unless the denominator and inspection method are defined.
Why These Characteristics Matter in Medical Components
The functional importance depends on the next operation and device design. Straightness can affect automatic feeding, laser positioning, insertion into a hub, alignment through a guide, bonding length and the ability to hold the tube in a fixture. Local ovality can affect press fits, seals, concentric assemblies, rotational alignment and available internal flow area.
These effects should be evaluated by the medical device manufacturer as part of design control. A geometrically tighter tube is not automatically safer or more suitable. Unnecessarily restrictive requirements can increase straightening, handling and inspection work without improving the finished device. The drawing should control the features that have a demonstrated relationship to assembly or function.
How to Specify Tube Straightness
Start with the condition in which the tube will be used. A short cut tube, a long shipping length and a coil cannot share the same inspection setup. If the supplied tube will be laser cut into short sections, the required straightness over the process feed length may matter more than the bow across the full shipping length.
A straightness note should normally address the following:
- The length or span over which deviation is evaluated.
- Whether the requirement applies to the tube axis, an outside surface line or another defined feature.
- How the tube is supported and whether it is allowed to rotate during inspection.
- Whether end regions are included or excluded.
- The acceptance value and units.
- The measurement method, gauge or agreed reference setup.
- The delivered temper, cut condition and packaging state.
Expressions such as “perfectly straight” or “no visible bend” are not suitable acceptance criteria unless an approved visual standard and viewing method are supplied. If a straight edge and feeler gauge are used, define the straight edge length, contact orientation and maximum permissible gap. If rollers and a dial indicator are used, define support spacing and whether the reported value is total indicator movement or a calculated axis deviation.
How to Specify Roundness or Ovality
The buyer should first decide whether the functional need is true cross-sectional roundness or a simpler two-point ovality limit. A micrometer measurement at several angular positions can identify maximum and minimum OD, but it does not reconstruct the full profile. A roundness instrument or optical system may provide richer form information, although access, fixturing and part size can limit the method.
For ovality, state the equation. One common absolute convention is:
Ovality = Dmax – Dmin
A percentage convention may be written as:
Ovality percentage = (Dmax – Dmin) / defined reference diameter x 100
The “defined reference diameter” must be named as nominal diameter, mean measured diameter or another agreed value. Also state the cross-section location, number of angular readings and measurement force. Thin-wall tubing can deform under a contact gauge, so excessive force can create a misleading result.
OD, ID and Wall Thickness Must Be Read Together
OD ovality does not establish ID roundness. A tube may have a reasonably round OD while the bore is displaced, or both surfaces may be oval in different directions. Wall thickness variation and concentricity can therefore matter when the tube must fit over a component, receive a wire or preserve a defined flow area.
Before adding several geometric controls, decide which dimensions are directly controlled and which are reference values. The guide to specifying OD, ID, wall thickness and tolerance for medical tubing explains why tolerance accumulation should be reviewed before the RFQ is approved.
Internal geometry may also be difficult to measure without sectioning or specialized equipment. If ID form is critical, the buyer and supplier should agree whether the evidence comes from an optical section, internal gauge, air measurement, computed method, process coupon or another validated approach. Destructive preparation must be described because cutting and mounting can alter a thin cross-section.
Inspection Methods and Their Limits
| Method | Useful for | Points to define |
|---|---|---|
| Straight edge and feeler gauge | Practical bow comparison over a stated length | Support, contact line, span, rotation and gap interpretation |
| Rollers or V-blocks with indicator | Runout-related evaluation and comparative straightness | Support spacing, rotation, indicator position and reported calculation |
| Optical comparator or vision system | Profile, local form and short-part alignment | Magnification, edge detection, datum, field of view and calibration |
| Micrometer at multiple angles | Maximum and minimum OD for a stated ovality calculation | Contact force, angular positions, section location and formula |
| Roundness measuring instrument | Detailed cross-sectional form | Fixturing, filter settings, reference circle and evaluation method |
| Prepared cross-section | ID shape, wall distribution and concentric relationship | Cutting, mounting, polishing, image scale and preparation influence |
No method is automatically correct for every size. Measurement resolution should be suitable for the tolerance, and the gauge must not significantly deform the part. The inspection record should identify the equipment or method, calibration status, location, orientation and actual result.
Manufacturing and Handling Can Change the Result
Cold drawing, annealing, intermediate sizing, straightening, centerless grinding, cutting and secondary forming can influence final geometry. Straightening may improve bow but can introduce residual stress or local marks if the process is not controlled. Cutting can affect the end region, while aggressive clamping can flatten a thin wall.
Packaging also matters. Long, slender tubes can pass final inspection and then bend when bundled too tightly or allowed to move during transport. The drawing and purchase order should make clear whether geometry is accepted before packaging or must be maintained in the delivered state. The supplier and buyer should agree on separation, support, bundle size and handling where shipping deformation is a known risk.
Build a Sampling Plan Around the Process
A sample plan should reflect the production route, lot definition, length and functional risk. One reading from one end of one tube does not describe an entire lot. If the process could vary along a draw length or between cut positions, samples may need to represent different locations. If the check is destructive, the plan should identify how test pieces relate to delivered parts.
For a first order, connect geometric results to the approved drawing and identified samples. The medical tubing first article inspection checklist provides a broader framework for revision control, material traceability and measurement records.
Routine production records should use the same definitions as the approved first article. Changing from an optical method to a hand measurement, or changing the support span, can create results that cannot be compared directly even when the parts have not changed.
A Practical Drawing and RFQ Checklist
- Identify the material grade, temper and supplied tube condition.
- State nominal OD, ID or wall thickness and their tolerances.
- Define whether straightness applies to the axis or a surface element.
- State the straightness inspection span, support and end exclusions.
- Define roundness or ovality and provide the calculation formula.
- Name the cross-section locations and number of angular readings.
- Set expectations for measurement force on thin-wall parts.
- Identify sample quantity, lot coverage and required records.
- Describe packaging needed to preserve the accepted geometry.
- Provide the downstream assembly or process constraint when possible.
These details should accompany quantity, cut length, end condition, cleanliness and documentation requirements. The medical tubing RFQ checklist can help buyers prepare a complete inquiry.
Questions to Ask a Potential Supplier
- Which manufacturing steps control straightness and local cross-sectional form?
- What inspection method is proposed for the specified diameter, wall and length?
- Can the method measure the ID requirement directly, or is a prepared section required?
- How will measurement force and part support be controlled?
- Which locations and angular positions will be included in the report?
- How are samples linked to the raw material and production lot?
- How will packaging protect accepted long tubes during transport?
- Which drawing notes need clarification before a capability statement is made?
Healsmed reviews custom requirements against the material, dimensions, length, inspection method and production route. The medical stainless steel capillary tube capability page provides the main product overview, but final feasibility should be based on the controlled drawing.
Frequently Asked Questions
Is ovality the same as roundness?
No. Ovality usually compares maximum and minimum diameters at a cross-section. Roundness evaluates departure of the full profile from a reference circle. The methods can produce different information and should not be substituted without agreement.
Can a tube pass OD tolerance and still fail ovality?
Yes. Individual measured diameters may fall within the OD limits while their difference exceeds a separately specified ovality limit. Conversely, a nearly round tube can still be above or below the allowed OD range.
Does straightness over the full length control every short section?
Not necessarily. A full-length bow requirement and a local straightness requirement describe different conditions. If both affect processing, the drawing should provide separate spans and acceptance values.
How should thin-wall tubing be measured without flattening it?
The measurement method and contact force should be selected for the material, diameter and wall thickness. Optical methods, controlled-force gauges or agreed sectioning may be considered, but suitability must be confirmed for the specific part.
Do straightness and ovality prove that tubing is medical grade?
No. They are dimensional characteristics. Medical suitability also depends on material specification, traceability, surface condition, cleanliness, manufacturing controls, intended use and the device manufacturer’s regulatory evaluation.
Conclusion
A useful tubing specification separates straightness, roundness and ovality instead of using them as general words for quality. It connects each requirement to a span or cross-section, datum, formula, measurement method, sampling plan and delivered condition. That clarity helps medical device buyers compare suppliers and reduces avoidable disagreement during inspection.
Send the drawing, material, OD, ID, wall, cut length, geometry requirements and proposed inspection method through the Healsmed RFQ page for a manufacturability review.
Healsmed
Leading Stainless Steel Capillary Tube Factory. 1,400+ standard sizes IN STOCK & ready to ship worldwide! High precision, factory-direct price.